
 English
 Español
 русский

Hydraulic Shock Absorber Tube – EN 10305-2 E235+N, Cold Drawn Welded Precision Steel Tube Ø40 x 2mm
Our Hydraulic Shock Absorber Tube is manufactured to EN 10305-2 standards using
Content
EN 10305-2 cold drawn welded tube is the precision tube behind many hydraulic cylinders, telescopic stages, shock absorbers, drive shafts, and compact mechanical assemblies. If you work in fluid power or machine building, you have probably handled a length of it without knowing the standard number. This guide explains what EN 10305-2 actually covers, how E235 and E355 behave, which delivery conditions matter, and how to specify the right tube without overpaying for unnecessary processing.
EN 10305-2 is the part of the European EN 10305 standard that covers welded cold drawn precision steel tubes. Production begins with steel strip or coil, which is formed and electric resistance welded into a hollow. The welded tube is then cold drawn over a mandrel or plug to its final size. That second step is the difference: the weld gives you a consistent wall and long lengths, while cold drawing gives you tight dimensions, a smoother surface, and better concentricity than a plain welded tube.
People sometimes use CDW tube, DOM tube, and EN 10305-2 tube interchangeably. They are close, but not identical. DOM describes the manufacturing route; EN 10305-2 defines the technical delivery conditions. The table below shows where the three main EN 10305 parts sit.
| Standard part | Manufacturing route | Common tube name | Typical applications |
|---|---|---|---|
| EN 10305-1 | Seamless, cold drawn | CDS hydraulic tube | High-pressure hydraulic cylinders, critical fluid power |
| EN 10305-2 | Welded, then cold drawn | CDW / DOM precision tube | Hydraulic cylinders, telescopic cylinders, shock absorbers, drive shafts |
| EN 10305-3 | Welded, then cold sized | ERW precision tube | General mechanical parts, conveyor rollers, low-pressure duties |
The practical point is simple. When a welded tube needs hydraulic-grade dimensional control and a clean inner diameter, EN 10305-2 is usually the most cost-effective route. When the application demands a seamless body for very high pressure or specific code requirements, EN 10305-1 takes over.
Cold drawing improves more than the outside diameter. It refines wall thickness variation, improves straightness, and creates a denser surface that resists wear and corrosion better than an as-welded finish. In a well-controlled line, the weld seam is drawn and blended into the wall so that the tube behaves as a uniform component rather than a welded shell with a weak line.
For hydraulic service, the inner diameter is where the real performance lives. Seal life, leak paths, and stick-slip behavior all depend on ID finish. A bore that looks smooth under shop light may still have axial marks, ovality, or a roughness peak that cuts a seal lip. That is why we regularly supply honed and SRB tube with H8 ID tolerance and Ra0.4 mirror finish. If you have ever replaced a cylinder seal too early, our article on why hydraulic cylinder seals keep failing explains the ID finish factors in more detail.
The two grades you will meet most often in EN 10305-2 are E235 and E355. E235 is a lower-carbon grade with good formability and weldability. It is a sensible choice for general precision tube, lower-pressure cylinders, and parts that will be bent or machined. E355 raises the minimum yield strength to 355 MPa and is common in hydraulic cylinder barrels, telescopic sections, and higher-load mechanical parts where wall thickness must stay economical.
The grade alone does not define the tube. The delivery condition controls strength, ductility, residual stress, and machinability. EN 10305-2 uses symbols that are easy to miss on a purchase order, so confirm them before quoting.
If you are not sure, tell us the final operation. A tube that will be honed, skived, or threaded usually needs a different condition than a tube that goes straight into a welded assembly.
EN 10305-2 sets tolerances for outside diameter, inside diameter, wall thickness, length, straightness, and end squareness. Cold drawn welded tube normally holds tighter OD and wall tolerances than EN 10305-3 cold-sized tube, and it can be supplied with controlled ID for hydraulic use. Typical ID tolerances include H9 for general service and H8 for cylinder bores, depending on size and process route. Straightness of 0.5 mm per meter or better is achievable for precision grades.
| Grade | Minimum yield strength ReH (MPa) | Typical tensile strength Rm (MPa) | Typical elongation A (%) |
|---|---|---|---|
| E235 | 235 | 470-630 | 18-24 |
| E355 | 355 | 640-820 | 14-20 |
These ranges shift with delivery condition. A +C tube will sit at the higher end of tensile strength and the lower end of elongation. An +A or +N tube will be softer and more ductile. For critical pressure or fatigue applications, mechanical testing and dimensional inspection should be part of the purchase specification, not an afterthought.
Hydraulic and pneumatic cylinders are the classic home for this tube. It is also used in telescopic cylinders, shock absorber bodies, drive shafts, conveyor rollers, and precision mechanical assemblies where a seamless tube would add cost without adding value. The common thread is a need for consistent dimensions, a clean bore, and reliable weld quality in long production runs.
For general CDW and DOM supply, our EN 10305-2 E235/E355 cold drawn welded tube covers the standard range in both grades and multiple delivery conditions.
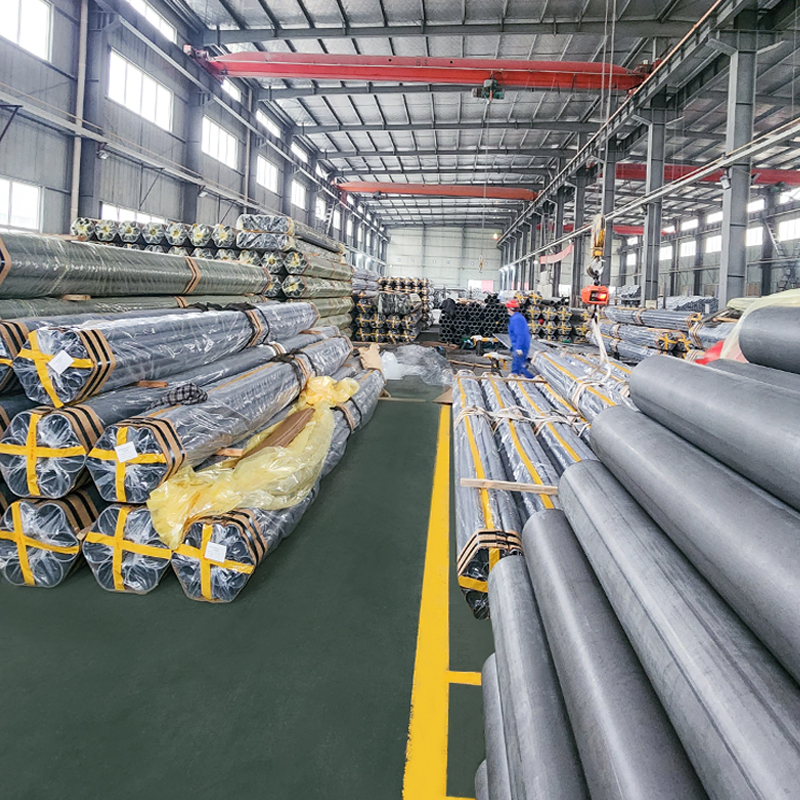 Cold Drawn Welded Steel Tube (CDW) En10305-2 Grade E235 E355 E460Precision Cold Drawn Welded Steel Tubes (CDW) – EN 10305-2 E235 E355 High-Tolerance Steel Tubing for Hydraulic, Automotive Mechanical Engineering Suao Metal manufactur...View Product →
When the tube is going into a hydraulic cylinder barrel, we also produce EN 10305-2 E355 cold drawn welded tube specifically for cylinder service, with the dimensional and surface controls that barrel makers expect.
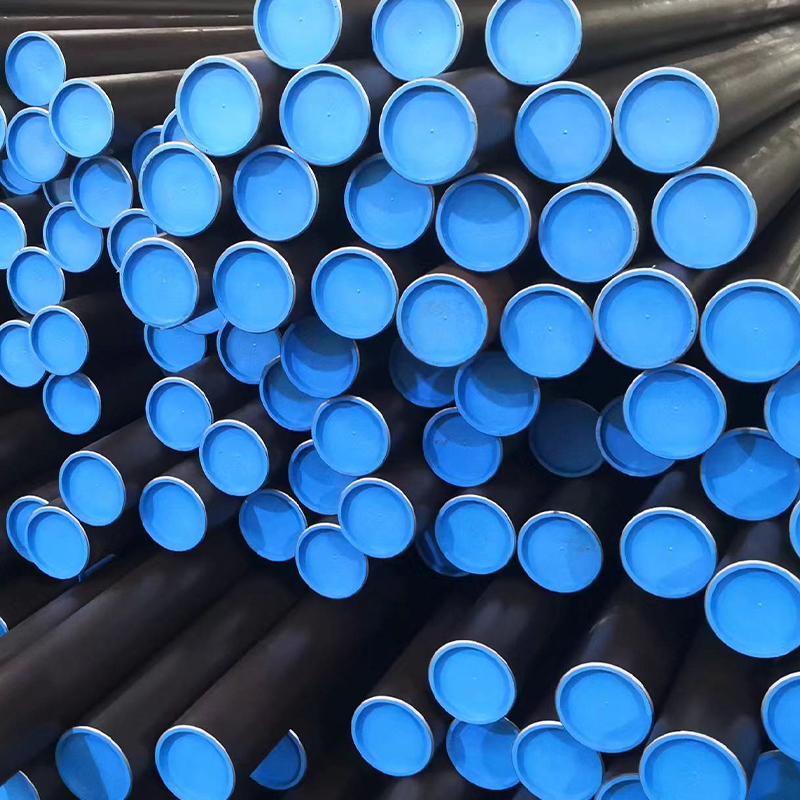 Hydraulic Cylinder Tube – Cold Drawn Welded Steel EN 10305-2, E355, For Honing & SRBOur Hydraulic Cylinder Tubes (CDW) are produced according to EN 10305-2 E355, using high-quality welded steel pipes that are further cold drawn to improve accuracy, su...View Product →
For bores that will see reciprocating seals, honed and SRB tube takes the same EN 10305-2 E355 base and brings the ID to H8 with Ra0.4 mirror finish.
 Honed & SRB Tube – EN 10305-2 E355 H8 Ra0.4, Mirror ID Finish for Hydraulic Cylinder BarreOur EN 10305-2 Cold Drawn Welded (CDW) Honed SRB Tubes are precision-processed to deliver mirror-like internal finishes (Ra ≤ 0.4 μm) and H8 tolerance, making them ide...View Product →
At our mill, EN 10305-2 production starts with certified steel strip. We form and ERW weld the hollow, then inspect the weld online before cold drawing. Drawing reductions, lubrication, and mandrel or plug selection are set for each size so that the weld is properly consolidated and the wall remains uniform. After drawing, tubes are annealed or stress relieved as required, straightened, cut, and inspected.
Quality control covers chemistry, weld integrity, OD, ID, wall thickness, straightness, surface condition, and mechanical properties. For honed tube, we measure the bore with precision gauges and verify surface roughness with profilometers. We can also supply phosphated, oiled, or e-coated tube when the parts need corrosion protection before assembly. The goal is not just to meet a standard on paper, but to deliver a tube that behaves the same on the first day and after ten thousand cycles.
To get an accurate quote and the right tube, share these details with your supplier:
The more you tell us, the lower the risk of a costly mismatch. Small batches and custom sizes are welcome. We regularly produce non-standard dimensions, special shapes, and pre-machined components that go beyond a simple tube order.
EN 10305-2 cold drawn welded tube is not a commodity once it enters a hydraulic cylinder or a precision assembly. Grade, delivery condition, ID finish, and weld quality all decide how long the final product lasts. Choose the specification for the job, verify the mill certificate, and work with a supplier who can explain the process instead of just quoting a price. You can explore our precision steel tube range to see the sizes and finishes we run every day.
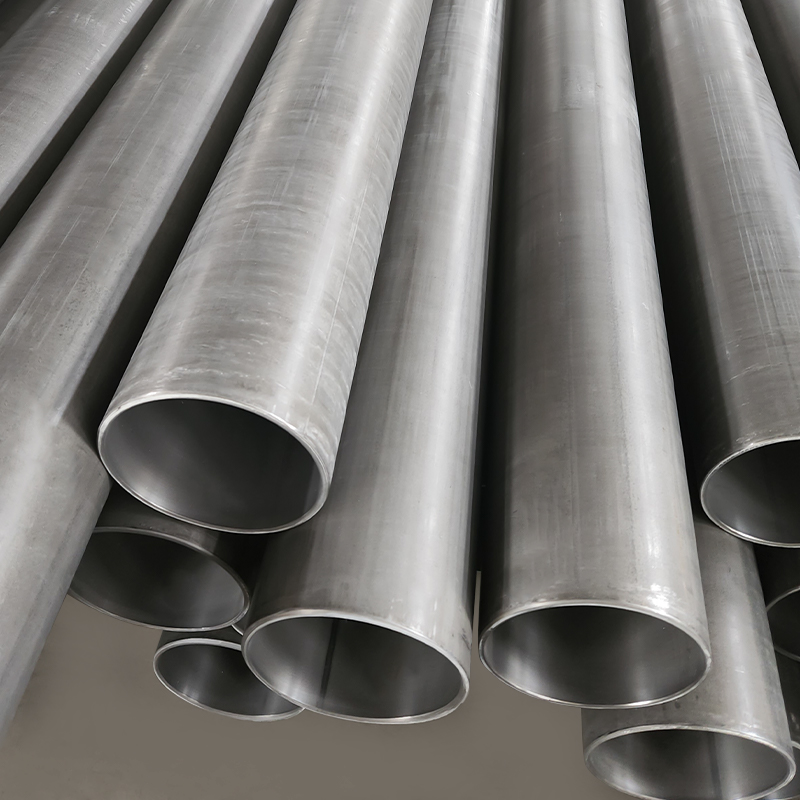
Our Hydraulic Shock Absorber Tube is manufactured to EN 10305-2 standards using
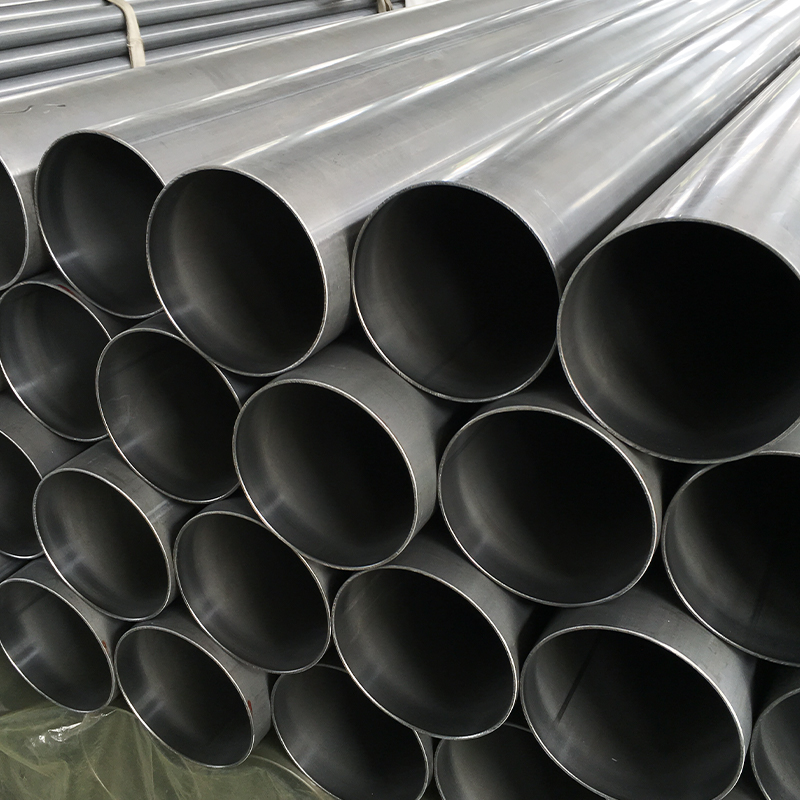
Our Seamless Shock Absorber Tubes are manufactured to EN 10305-1 using high-qual...
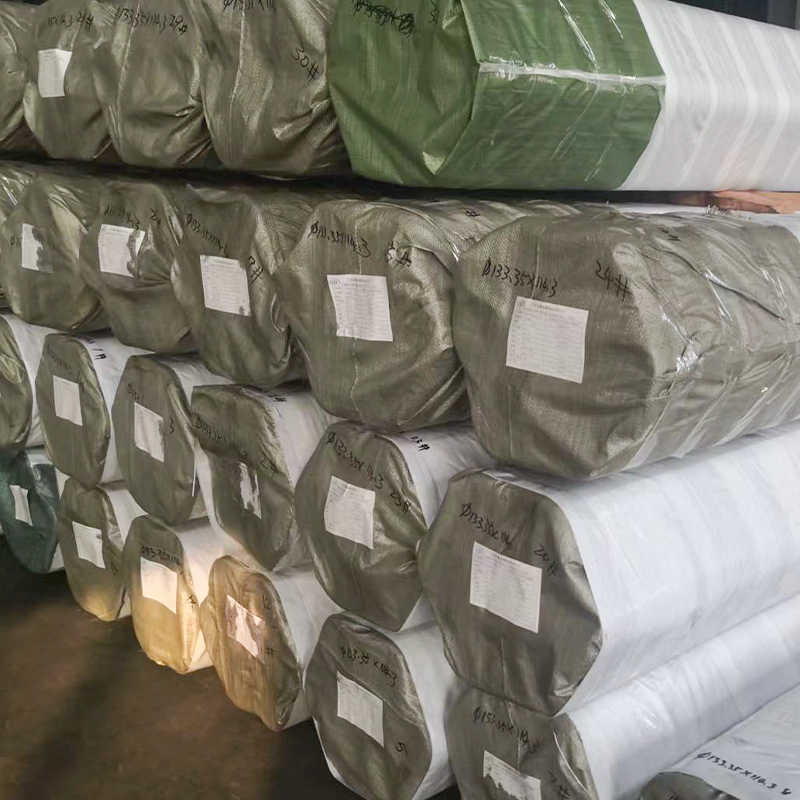
Our Hydraulic Cylinder Tubes (CDW) are produced according to EN 10305-2 E355, us...
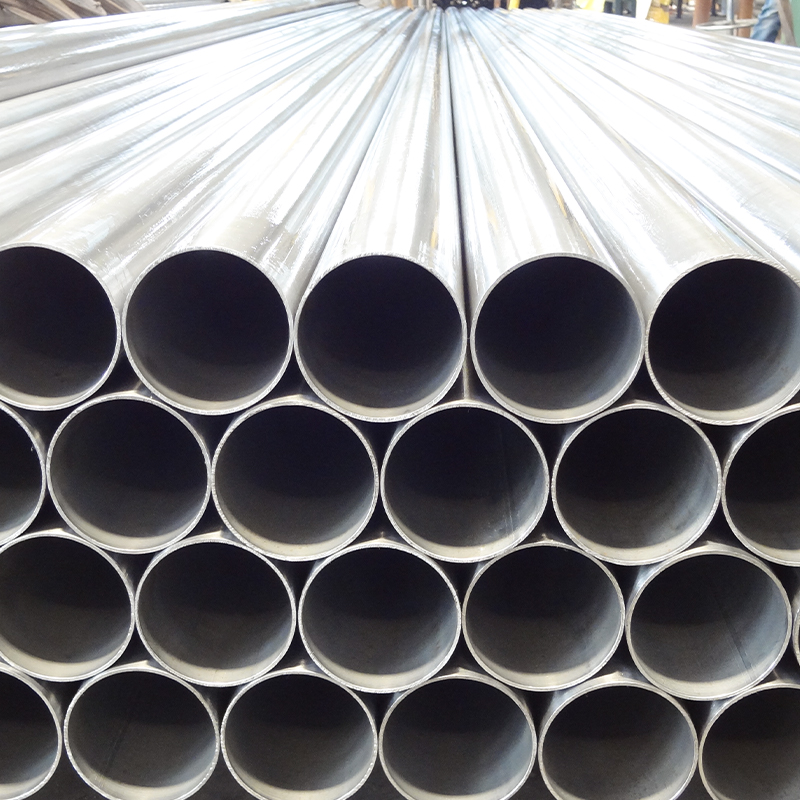
Precision Cold Drawn Welded Steel Tubes (CDW) – EN 10305-2 E235 & E355High-T...
Our Welded Hydraulic Tubes are produced from cold-drawn or ERW-welded strip stee...
Our Hydraulic Shock Absorber Tubes are manufactured using the Cold Drawn Welded ...


